Showing all 2 results

Chemical Hose Manufacturer

Rentone Hose is one of the major chemical hose manufacturers in China. As a reliable chemical hose supplier, we offer premium-quality chemical hoses to customers worldwide. Our factory is equipped with advanced equipment. We have multiple production lines capable of producing various industrial chemical hoses.

Rentone Hose produces industrial chemical hoses in a diverse range of types, specifications, and colors. Our product portfolio includes chemical-resistant hoses, chemical-spraying hoses, chemical-transfer hoses, braided chemical hoses, high-pressure chemical hoses, UHMWPE chemical hoses, chemical suction and discharge hoses, and food-grade chemical hoses. Our UHMWPE chemical hose is a suction and discharge hose with excellent chemical corrosion resistance and high abrasion resistance. It can transport common acids, alkalis, salt solutions, and organic solvents, and is widely used in the chemical, pharmaceutical, and tank truck industries.

Furthermore, we offer customization services. You can provide us with details regarding your operating environment, media, temperature and pressure parameters, and coupling requirements, and our technical team will design a chemical hose solution specifically for your needs.

Get a Free Quote


Specifiction

Item UHMWPE Chemical Hose PTFE Chemical Hose Rubber Chemical Hose Chemical Composite Hose
Inner Diameter 1/2″ - 4″ 1/4″ - 2″ 1/2″ - 6″ 1″ - 12″
Working Pressure 6 - 10 bar 10 - 16 bar 4 - 10 bar 5 - 10 bar
Burst Pressure ≥ 18 - 30 bar ≥ 30 - 64 bar ≥ 12 - 30 bar ≥ 15 - 30 bar
Temperature Range -40°C to +100°C -70°C to +260°C -40°C to +80°C -30°C to +80°C
Inner Tube Material UHMWPE PTFE EPDM / NBR PP / PTFE film composite
Reinforcement Textile braid / steel wire Stainless steel braid Textile braid / steel wire Helix wire + fiber + film layers
Cover Material Abrasion-resistant rubber Stainless steel braid / rubber cover Weather & abrasion resistant rubber PVC coated fabric
Chemical Resistance Very Good Excellent Medium - Good Good
Flexibility Good Medium Excellent Very good
Typical Application Chemical plants, wastewater Pharma, high purity chemicals General industrial fluids Tank trucks, port loading/unloading
Standards EN 12115 / ISO 3821 EN 12115 / FDA options SAE J517 / ISO standards EN 13765

Chemical Hose Constructions

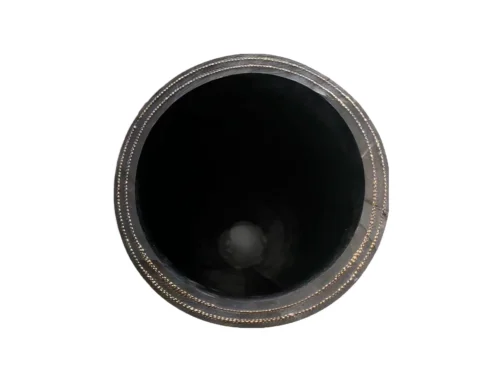
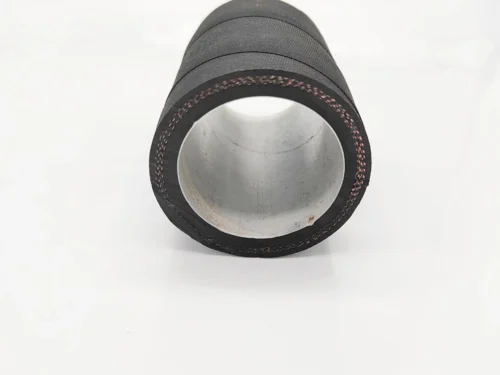
  • Inner Tube: Chemical resistant EPDM, smooth finish, black color
  • Reinforcement Layer: Synthetic cord with steel helix embedded
  • Outer Cover: Black EPDM, chemical and weather-resistant
  • Working Temperature Range: -40°C to +100°C
Get A Quote

Features of Chemical Hoses

  • Exceptional resistance to various chemicals and solvents
  • Excellent resistance to wear and tear, weathering, and UV light
  • Good mechanical strength
  • Excellent flexibility and bending radius
  • Highly durable and flexible
Get A Quote
Chemical-Hose-Manufacturer-rentone-hose

Testing Standard of Industrial Chemical Hoses

Our chemical hoses are manufactured in strict accordance with ISO 1823 standards and industry quality system requirements. Before leaving the factory, our industrial chemical hoses undergo rigorous pressure, burst, impulse, and chemical corrosion resistance testing to ensure long-term, stable operation under complex working conditions, providing safety and reliability. Designed with a 4:1 safety factor, our hoses meet the safety demands of the pharmaceutical, chemical, and food industries.

Get A Quote

Types of Chemical Resistant Hoses

Chemical hoses can be made in different types. Each is tailored to meet specific requirements and deal with varying types of chemicals. Some common types of industrial chemical hoses are as follows:

UHMWPE-Chemical-Hose

UHMWPE Chemical Hose

UHMWPE chemical hoses are made of ultra-high molecular weight polyethylene (UHMWPE). It has excellent chemical resistance and abrasion resistance and is commonly used for conveying corrosive chemicals and fluids.

Get A Quote
PTFE-Chemical-Hose

PTFE Chemical Hose

These hoses are made of Polytetrafluoroethylene (PTFE) and possess superior chemical resistance, enabling them to withstand corrosive chemicals. PTFE hoses are widely used in the pharmaceutical and food processing industries.

Get A Quote
Rubber-Chemical-Hose

Rubber Chemical Hose

Rubber chemical hoses use EPDM and NBR synthetic rubber as the inner layer, which has good flexibility. Its cost is relatively low, and it is used for transporting mildly corrosive liquids in the chemical industry.

Get A Quote
Composite-Chemical-Hoses

Composite Chemical Hose

Composite chemical hoses are constructed from thermoplastic films, reinforcing fibers, and internal and external steel wire spirals, resulting in a lightweight structure. Suitable for large-diameter, high-flow applications, they are widely used for port loading/unloading and tanker discharge operations.

Get A Quote

Why Choose Us As Your Chemical Hose Supplier

Sophisticated Technology

The company has introduced advanced manufacturing equipment. We can manufacture top-quality chemical hoses and products to meet specific customer requirements.

Tailored Chemical Hose

We are capable of supplying various chemical hoses in different types and sizes. We can offer custom chemical hoses to meet other specifications.

Excellent Manufacturing Capabilities

The company has experience in the manufacturing and production of various chemical hoses. So, we can supply high-quality, affordable chemical hoses to meet customer expectations.

Get A Quote

Applications of Chemical Hoses

Chemical hoses can suction, discharge, and transfer various aggressive chemicals, abrasive materials, and hazardous substances in industrial applications. They are ideal choices for food and the manufacturing industry, chemical processing plants, etc.

Get A Quote

FAQs

A chemical hose can deliver various kinds of chemicals, liquids, and solvents safely and efficiently. It is made of flexible EPDM material to ensure no leakage or chemical reactions are caused.

Common uses of inner tube materials of industrial chemical hoses include UHMWPE, PTFE, FEP, and Viton.

UHMWPE (Ultra-High-Molecular-Weight Polyethylene) is a corrosion-resistant material commonly used in the chemical industry. It withstands low temperatures and is suitable for conveying media containing solid particles, such as silt, mineral slurries, and wastewater.

PTFE offers excellent chemical corrosion resistance and is suitable for conveying highly corrosive media, including strong acids, strong alkalis, and potent organic solvents. It operates stably in both low- and high-temperature environments; with its smooth inner wall and good flexibility, it is an ideal choice for the chemical, food, and pharmaceutical industries.

Another material is fluoroelastomer (FKM/FPM), a synthetic rubber containing fluorine atoms. It boasts excellent resistance to corrosion, high temperatures, and aging. Consequently, it is frequently used to convey media such as gasoline, diesel, acids, alkalis, fuels, and organic solvents.

The materials mentioned above are resistant to strong corrosion. Materials resistant to mild corrosion include neoprene, EPDM, NBR (nitrile rubber), and polyurethane. For media such as dilute sulfuric acid, water, or alcohols, EPDM is the preferred choice. For media such as petroleum products, hydraulic oil, or mineral oil, NBR or neoprene materials are preferred.
Our chemical hose fittings are primarily made of two materials: stainless steel and PP (polypropylene).

Stainless steel fittings are the most common type on the market. They offer excellent resistance to acids, alkalis, and corrosion, ensuring no rusting occurs during the long-term transport of chemical media. Stainless steel is highly rigid, resistant to deformation during installation, structurally stable, and offers a longer service life.

PP (polypropylene) is used in normal-temperature, low-pressure environments and in highly corrosive chemical environments. PP is lightweight, making installation easier.

1. Confirm the name, composition, and particle content of the chemical substance being conveyed.

2. Consider the operating environment and ambient temperature.

3. Ensure the hose's working pressure exceeds the system pressure.

4. Determine the application: chemical transfer hose vs. chemical suction and discharge hose.

5. Special features: anti-static design.

6. Compliance with relevant chemical hose standards.

At Rentone, we use the STAMPED selection method to help you choose the correct chemical hose. The seven letters stand for: S (Size), T (Temperature), A (Application), M (Media), P (Pressure), E (End Connections), and D (Delivery).

UHMWPE chemical hoses outperform PTFE in terms of flexibility, abrasion resistance, and overall cost-effectiveness.

UHMWPE is 3-5 times more abrasion-resistant than PTFE and will not crack even with frequent dragging. PTFE has relatively weak abrasion resistance and is prone to wear and leakage in rough surface environments.

Compared to PTFE, UHMWPE has superior flexibility, making it easier to bend and handle during installation. It is also lighter and easier to transport.

UHMWPE hoses feature an embedded spiral steel wire. Even in a full vacuum environment, it will not deform or collapse, truly achieving bidirectional operation of negative-pressure suction and positive-pressure conveying.